
From robotic intelligence platforms to power conversion modules, explore our certified surface-mount, through-hole, and mixed-technology assemblies engineered for extreme duty cycles.
Understanding the geopolitical, logistical, and technical mechanics of the Pearl River Delta electronics cluster and how it delivers unmatchable velocity from NPI prototype to mass deployment.
In modern high-velocity electronics hardware manufacturing, time-to-market is not merely a KPI; it is the ultimate determinant of commercial viability. Located in the core of Shenzhen's Bao'an and Nanshan tech corridors, our manufacturing facilities harness what global hardware engineers refer to as the "Hardware Silicon Valley Ecosystem". Unlike fragmented manufacturing regions across Western territories or emerging secondary offshore hubs, Shenzhen consolidates every single tier of the electronics bill of materials (BOM) within an extraordinary 1-hour logistics radius.
This ecosystem superiority manifests in concrete engineering agility. When a complex multi-layer HDI board requires custom dielectric prepregs, high-Tg Rogers or Isola substrates, ultra-fine-pitch BGA packaging (down to 0.3mm pitch), or precision passive arrays (01005 passives), prototype fabrication and raw material procurement occur in hours rather than weeks. The proximity to the world's dense electronic component distribution matrix—including direct franchised factory agents, domestic silicon design houses, and the premier Huaqiangbei spot hub—allows us to eliminate typical 6-to-12-week overseas component procurement lead times for vital active and passive nodes.
Rapid engineering verification via dedicated NPI (New Product Introduction) lines. Fast-track prototype SMT turnaround within 24 to 48 hours following BOM validation, enabling hardware engineers to iterate design revisions five times faster than traditional regional assemblers.
Direct partnerships with original semiconductor manufacturers and audited Tier-1 franchise distributors (including Arrow, Avnet, Mouser, and DigiKey). Over 500,000 SKUs held in temperature/humidity-controlled bonded warehouses ensuring zero counterfeit risk.
Complete elimination of multiple vendor markups. From bare copper fabrication (FR4, Rigid-Flex, MCPCB, Rogers, PTFE) through SMT, automated optical inspection (AOI), X-ray inspection, ICT, functional testing, and turnkey enclosure box build under one roof.
Adhering to IPC-A-610 Class 2 and Class 3 workmanship criteria, backed by internationally audited certifications across automotive, medical, industrial, and aerospace electronics.
Global procurement teams often confront legitimate concerns when auditing overseas assembly providers: counterfeit silicon injection, solder voiding in critical BGA thermal planes, non-compliant flux residues, and vague material certifications. At Shenzhen STHL Electronics, quality governance is architected to eliminate systemic risks through strict adherence to internationally recognized frameworks.
Our operations are fully certified under IATF 16949 (Automotive Quality Management Systems), ISO 13485 (Medical Device Manufacturing), ISO 9001 (Standard Quality Assurance), and ISO 14001 (Environmental Lifecycle Control). Every production batch undergoes full traceable documentation: incoming component counterfeit screening using decapsulation and XRF elemental spectroscopy, Automated Optical Inspection (AOI) verifying solder joint meniscus geometry, 3D inline Solder Paste Inspection (SPI) analyzing paste volume volume/height distribution, and 3D X-Ray Inspection (AXI) monitoring solder voiding percentages underneath non-visible BGA, QFN, and LGA thermal pads (guaranteeing void ratios strictly under 15%, well within IPC-A-610 Class 3 specifications).
| Certification / Framework | Target Industry / Application | Core Verification & Process Control Focus | MES Traceability Level |
|---|---|---|---|
| IATF 16949 | Automotive Powertrain, ADAS, HUD & In-Cabin ECUs | PPAP Level 3, APQP, FMEA risk mitigation, zero-defect process audits | Unit-level 2D QR Code & Serial ID |
| ISO 13485 | Class I/II/III Medical Devices & Surgical Diagnostics | Cleanroom assembly, bio-burden monitoring, rigid design history records (DHR) | Batch & Component Component Reel Lot |
| ISO 9001:2015 | Industrial Control, PoE, Automation & Computing | Standardized continuous improvement, calibrated metrology, supplier scorecards | Work Order & Operator Shift Tracking |
| RoHS & REACH Compliance | Global Consumer, IoT, Telecommunication Hardware | XRF heavy-metal screening (Pb, Cd, Hg, Cr6+), halogen-free material chemistry | Chemical Certificate of Analysis (CoA) |
| UL 94V-0 & UL 796 | Power Electronics, Energy Storage, High-Voltage Systems | Dielectric withstand, flammability retardance, thermal breakdown margins | Laminate Manufacturer Master Lot ID |
Hardware purchasing executives and VP-level engineering leaders require more than simple board stuffing. They demand comprehensive lifecycle de-risking.
Every submitted Gerber, ODB++, and centroid file undergoes detailed Design for Manufacturability (DFM) and Design for Assembly (DFA) audits. We detect copper clearance violations, tombstoning hazards, mismatched pad geometries, and insufficient test point coverage before a single dollar is spent on stencils.
Our security architecture is designed to protect overseas client IP. Comprehensive Non-Disclosure Agreements (NDAs) precede file exchange; firmware flashing occurs within isolated VLAN networks; engineering data is compartmentalized to prevent accidental disclosure or design leakages.
Silicon shortages and sudden end-of-life (EOL) announcements jeopardize volume production. Our 50+ professional hardware engineers cross-reference pin-compatible alternate active and passive parts, delivering 15% to 35% BOM cost optimizations without degrading functional tolerances.
Eliminate supplier lock-in bottlenecks. Whether your project requires a 5-unit proof-of-concept run or seamless high-volume scale-up exceeding 500,000 units annually, STHL processes your orders on unified production lines with uniform quality standards.
Exploring micro-pitch integration, high-frequency RF, high-current thermal management, and intelligent automated electronics manufacturing services.
The global electronics landscape is experiencing rapid evolutionary pressure driven by four key forces: Automotive Electrification (EV), Artificial Intelligence Edge Computing & Autonomous Robotics, Ultra-Dense High-Speed Interconnects (HDI), and Green/Lead-Free Industrial Standards. Modern PCBA manufacturers can no longer rely on conventional pick-and-place methodologies; production now requires advanced physical chemistry, precision thermal profilers, and sub-micron positioning equipment.
Equipped with high-precision Panasonic and Yamaha modular mounters, STHL accurately mounts components down to 01005 (0402 metric) chips and ultra-fine pitch BGAs (0.3mm ball pitch). Supported with blind/buried via micro-drilling, sequential lamination (Any-Layer HDI), and precise controlled-impedance routing (±5% tolerance) for high-speed signal integrity.
High-power distributed energy, PoE injectors, and motor servo controls generate substantial thermal density. We master thick copper assemblies up to 6oz, direct-bonded copper (DBC) ceramic substrates, aluminum IMS baseboards, and vacuum reflow soldering to minimize thermal resistance and eliminate solder voiding.
Harsh environments demand rigorous protective chemistry. Our automated selective conformal coating lines deploy acrylic, polyurethane, silicone, or UV-cure resins down to specified micron thicknesses. Coupled with robotic adhesive dispensing and potting, boards withstand moisture, salt spray, and extreme thermal cycling (-40°C to +125°C).
Detailed examination of how STHL PCBA solutions perform across critical industrial systems, commercial instrumentation, and next-gen embedded architectures.
Modern collaborative and warehouse automated guided vehicles (AGVs) require multi-axis motor driver boards combined with high-compute edge AI processing. STHL delivers rigid-flex assemblies housing complex BGA microprocessors, IMU motion sensors, and high-amperage MOSFET bridges capable of sustaining mechanical shock and continuous vibration.
Distributed solar, microgrid controllers, and high-voltage converters require strict high-creepage and clearance design. Our manufacturing process integrates specialized solder mask barriers, heavy copper tracing (3oz-6oz), and automated ICT/Hi-Pot (high-potential) dielectric testing up to 5,000V DC to ensure zero field arc-over risks.
Surgical navigation systems, real-time hemodynamic monitors, and diagnostic imaging equipment demand absolute precision. Operating under ISO 13485 cleanroom protocols, we fabricate high-reliability PCBA boards with comprehensive component traceability, flying probe verification, and functional burn-in stressing.
Sensors detecting corrosive exhaust gases or micro-pollutants must maintain long-term signal fidelity in outdoor environmental stations. We apply conformal coatings and inert encapsulation to preserve tiny sub-microvolt sensor signals from industrial chemical corrosion and atmospheric humidity.
Heads-Up Displays (HUD) and infotainment controllers must endure stringent thermal swings (-40°C to +105°C) and zero-defect automotive audit criteria. Using our IATF 16949 production line, we execute 100% 3D AOI, 3D X-Ray, and thermal shock chamber testing on every automotive work order.
Enterprise Network Video Recorders (NVR) and multi-channel security arrays involve high-bandwidth DDR3/DDR4/DDR5 routing, multi-gigabit Ethernet interfaces, and multi-stream storage buses. Our high-layer-count fabrication (up to 32 layers) ensures impedance control and low crosstalk across all high-speed parallel buses.
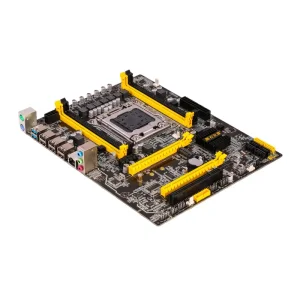
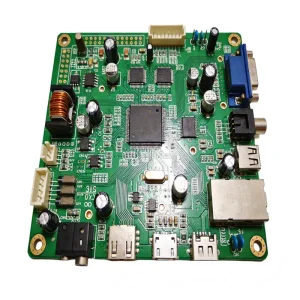
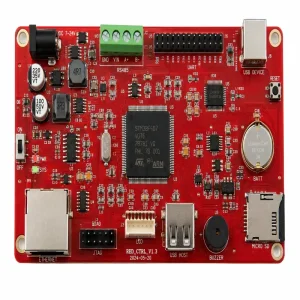
Continuing our specialized hardware lineup: security scanners, air data computers, smart hubs, and specialized power electronics built to exact customer specifications.
Detailed technical and commercial answers addressing common engineering inquiries, supply chain risk management, and qualification protocols.