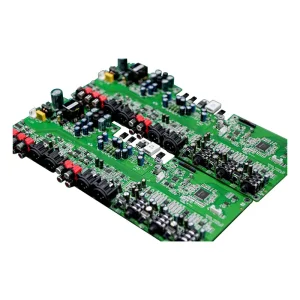
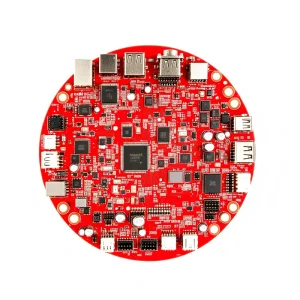
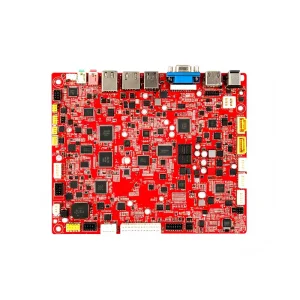
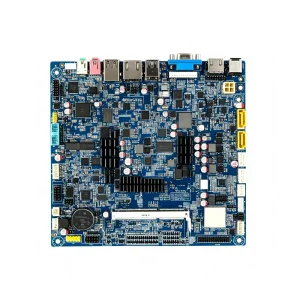
As Ghana continues to industrialize, the demand for stable, high-efficiency power management systems is skyrocketing. From telecommunications grid stability to rural solar power projects, we provide the backbone of reliable PCBA manufacturing.
Leveraging automated SMT lines and rigorous IATF 16949 quality standards, our Shenzhen facilities offer Ghana-based businesses the perfect blend of cost-efficiency and global-grade reliability.
We specialize in PCBA for DIN-rail industrial supplies, critical medical device power units, and renewable energy monitoring systems tailored for the harsh environmental conditions of the West African market.
A: Absolutely. Our 10,000sqm facility and capacity to handle no-MOQ prototypes up to mass production make us the ideal partner for scaling from pilot tests to full commercial rollout.
A: We utilize a strict multi-stage quality control process, including AOI and functional testing, coupled with full ERP/MES traceability for every component sourced.