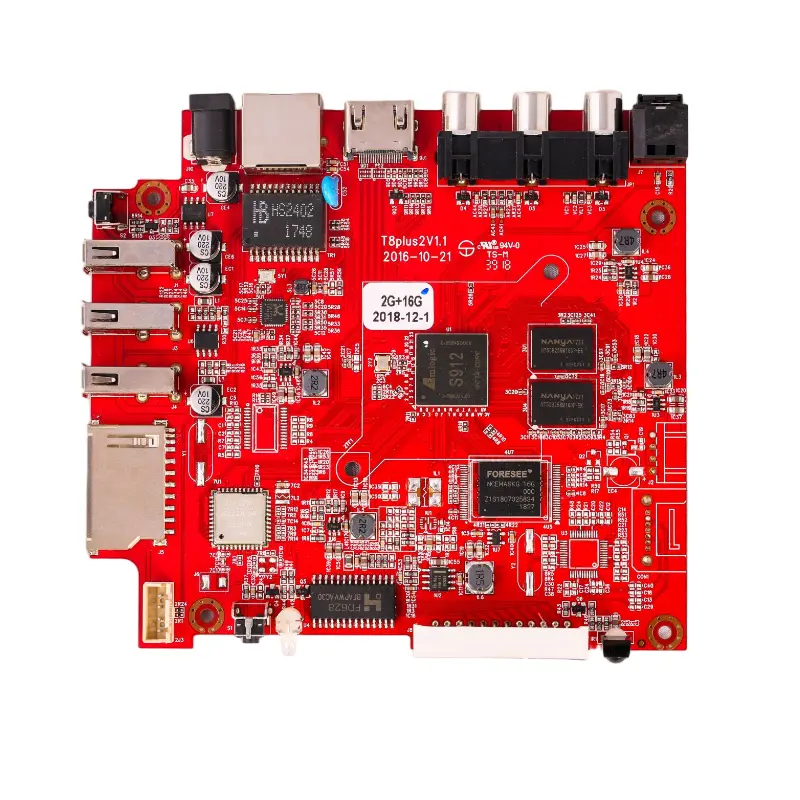
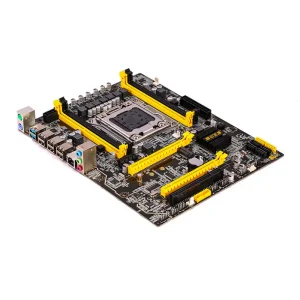
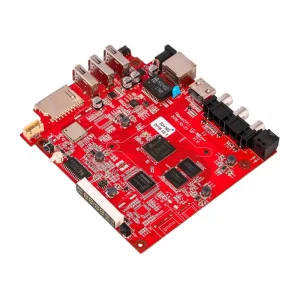
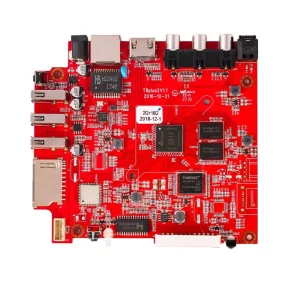
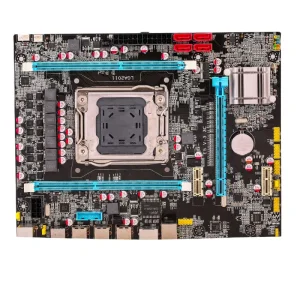
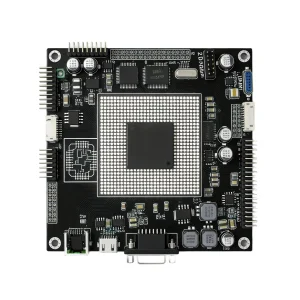
Industrial monitoring system PCBs serve as the operational backbone for continuous oversight of industrial equipment status and on-site environmental conditions. These high-reliability boards integrate multi-channel data acquisition modules to collect signals from temperature, pressure, vibration, and gas sensors, then process and convert raw data via embedded microcontrollers and signal-filtering circuits. Equipped with stable communication interfaces (Ethernet, RS-485, LoRa), they transmit real-time data to central control platforms or cloud systems. Engineered for harsh industrial settings, they feature anti-interference shielding, surge protection (up to 2kV), and wide temperature adaptability (-40°C to 85°C), effectively helping prevent equipment failures, optimize operational efficiency, and maintain strict safety standards across manufacturing plants, power facilities, and logistics warehouses.